Is Your Cooling Process Creating a Bottleneck in Your Production Line?
Your production line constantly stops, waiting for your cooling process to catch up. This bottleneck wastes time, increases labor costs, and disrupts your entire workflow, costing you money.
A cooling bottleneck is addressed by matching batch capacity, loading, unloading and downstream handling to the actual production rate. Automation may help some lines, but it is not a universal requirement; compare the complete workflow before adding equipment.
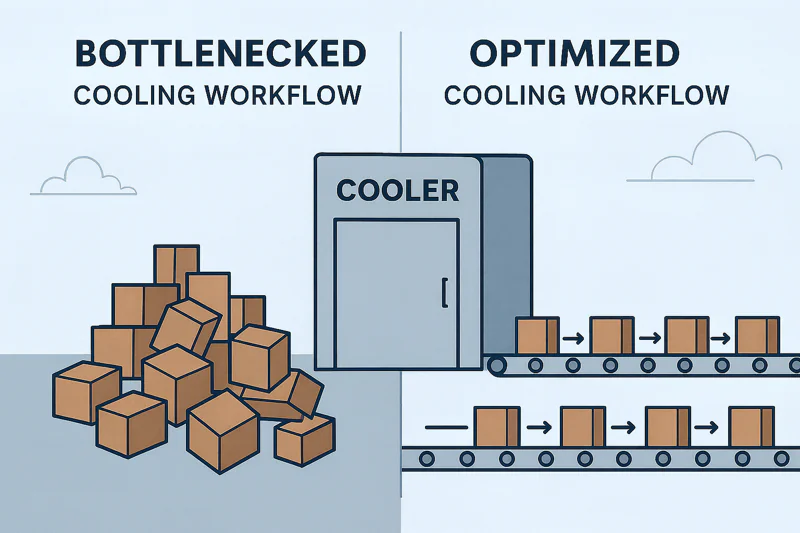
As a factory owner, I often see customers buy powerful equipment but fail to think about how it fits into their day-to-day operations. A vacuum cooler is incredibly fast, but if you spend 15 minutes manually loading it and another 15 unloading it, you’ve lost a huge chunk of your efficiency. The goal is to make the machine a seamless part of your flow, not an island that disrupts it. Planning the workflow is just as important as choosing the machine itself.
Where Should a Vacuum Cooler Go in Your Production Line?
You’ve invested in a new cooler, but where does it fit? Placing it wrong can disrupt your entire process, creating more problems than it solves and causing logistical nightmares.
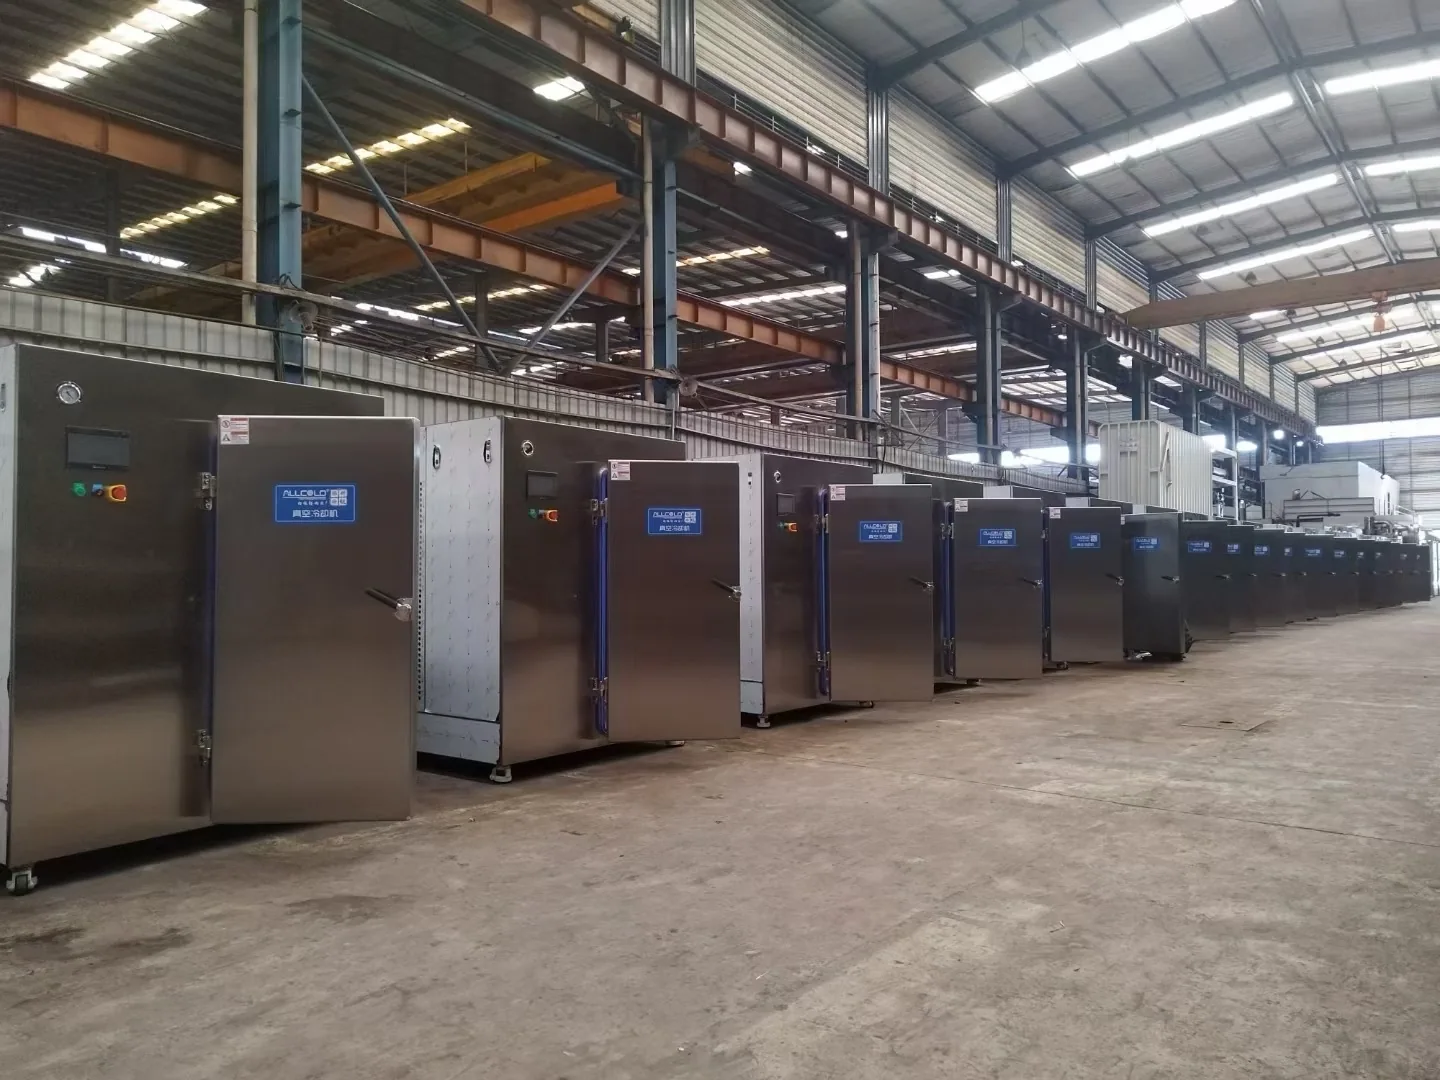
Allcold’s produce and food cooling ranges support configuration around pallets, trays or trolleys and the site’s production flow. This gives the layout discussion a concrete starting point: the load you already handle. Send the upstream release pattern and downstream capacity together. Conveyors, shared controls and data connections require their own agreed engineering and supply scope.
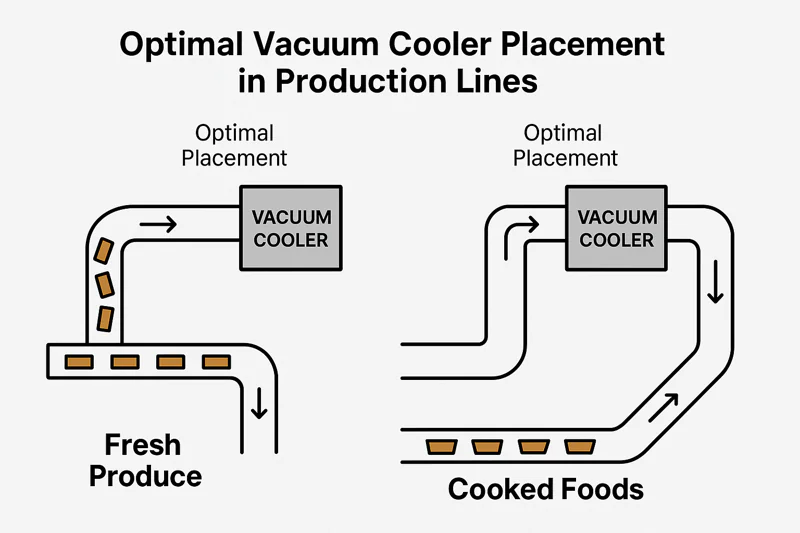
Locate the cooling stage according to the product’s handling requirements and the intended transfer into packing, chilling or storage. Confirm the actual sequence rather than applying one universal layout to produce and cooked foods.
Strategic Placement: Pre-Cooling vs. Post-Cooling
The correct placement of your vacuum cooler is the foundation of an efficient workflow. The decision depends entirely on your product. The guiding rule is always: cool it fast and cool it early.
For fresh produce, map the interval from harvest through cooling and cold storage, including packing where applicable. The sequence should be assessed for the actual commodity and pack. Precooling supports temperature management; it does not halt every form of deterioration or eliminate later handling risks.
For cooked food, define the cooling stage within the kitchen’s validated time-and-temperature process. Establish the required endpoint, transfer to any subsequent chilling stage and responsibility for product release. A generic machine cycle does not guarantee safe food or compliance.
| Application | Position to assess | Required check |
|---|---|---|
| Fresh produce | Between harvest handling and cold storage | Commodity, pack and transfer sequence |
| Bakery | After baking and before the intended next step | Product condition for slicing or packing |
| Cooked food | Within the validated cooling process | Required endpoint and subsequent chilling where needed |
How Can You Automate Your Cooler’s Loading and Unloading?
Your team spends too much time manually moving pallets in and out of the cooler with a forklift. This slow, labor-intensive process is a weak link, creating delays and safety risks.
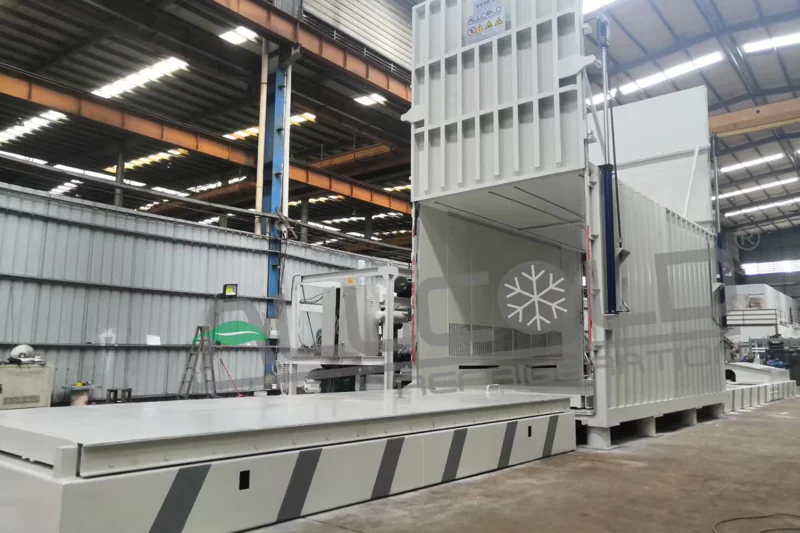
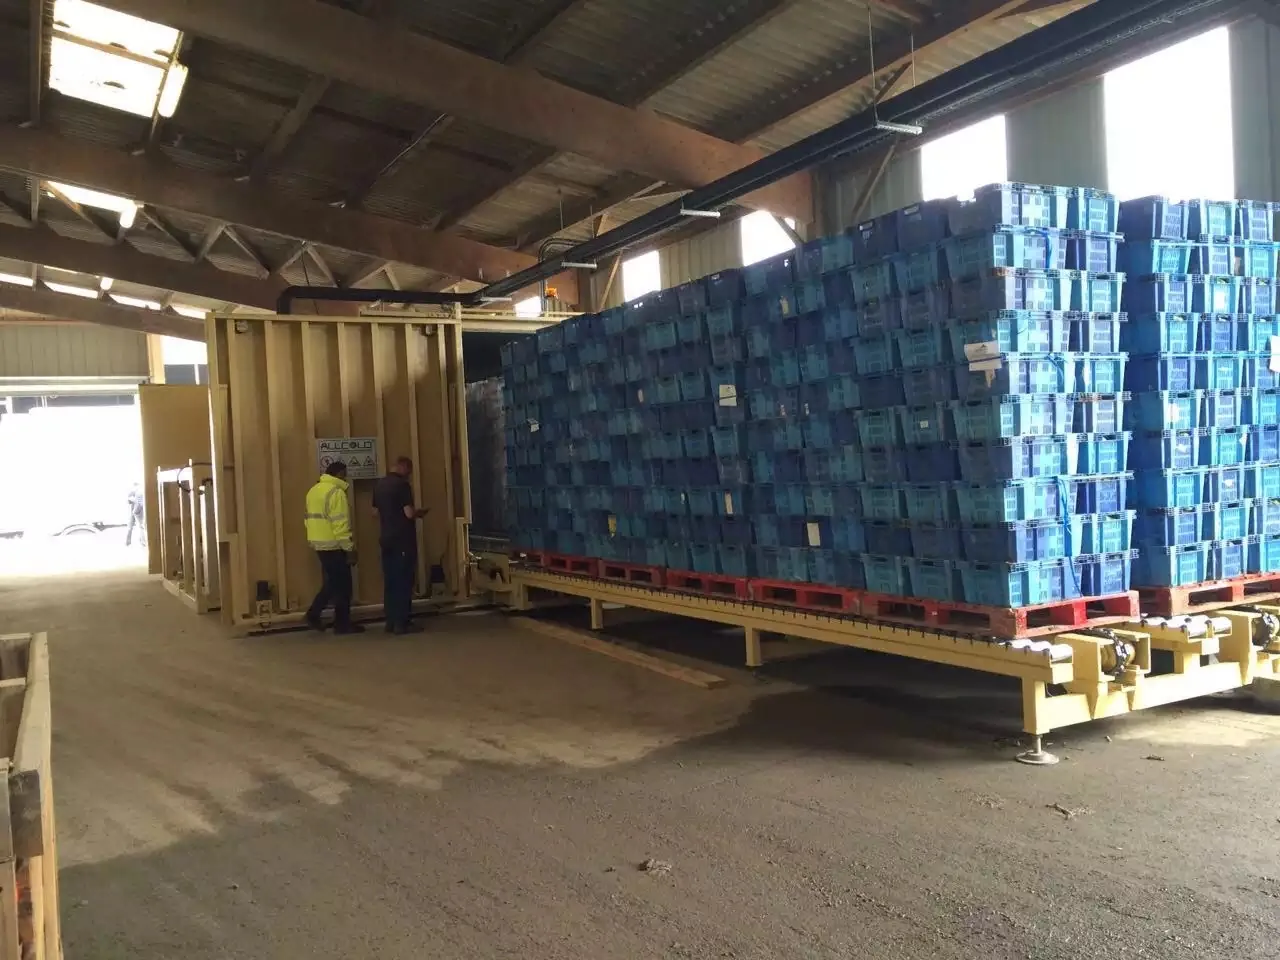
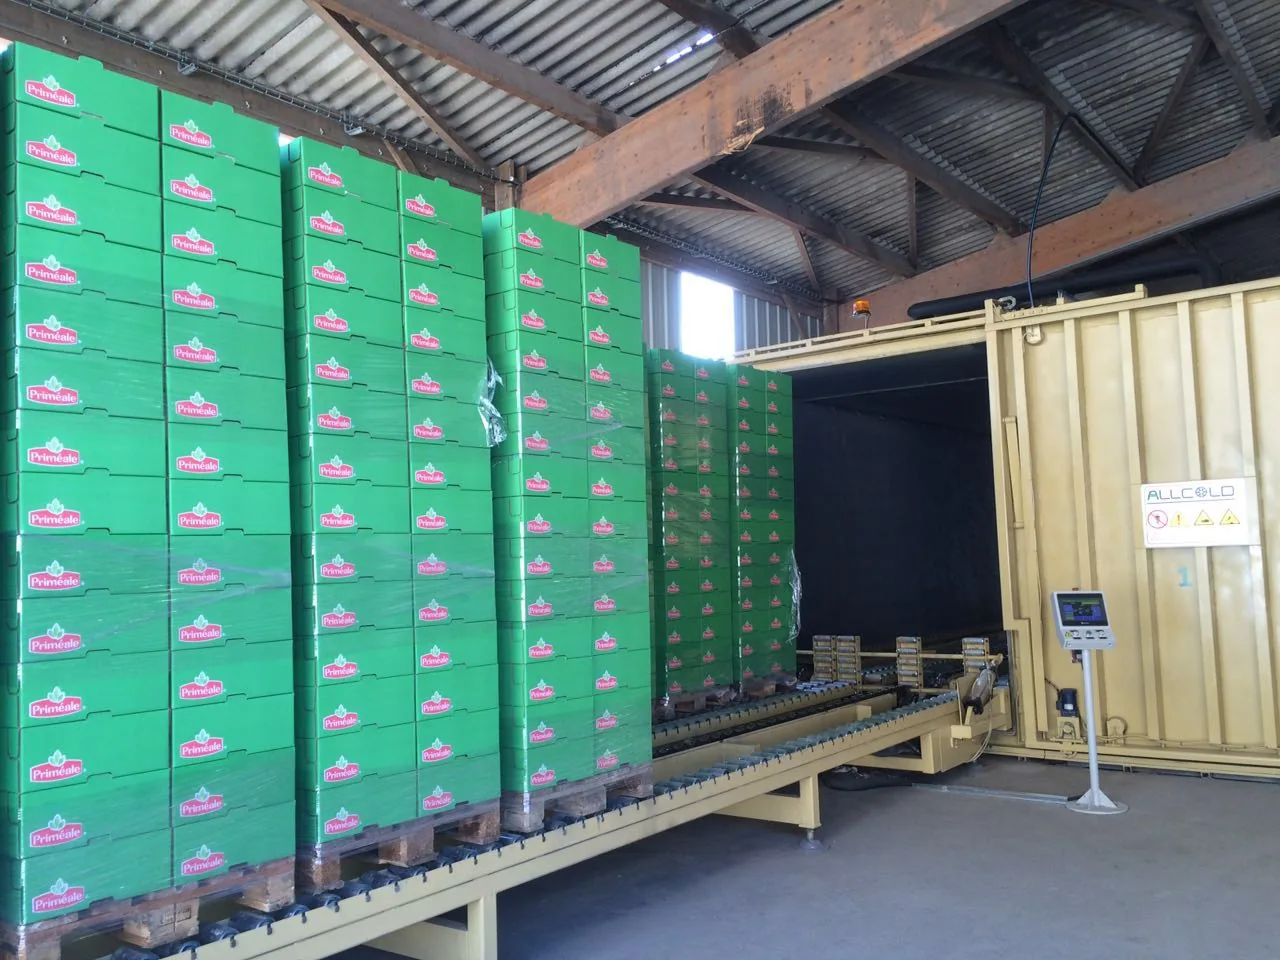
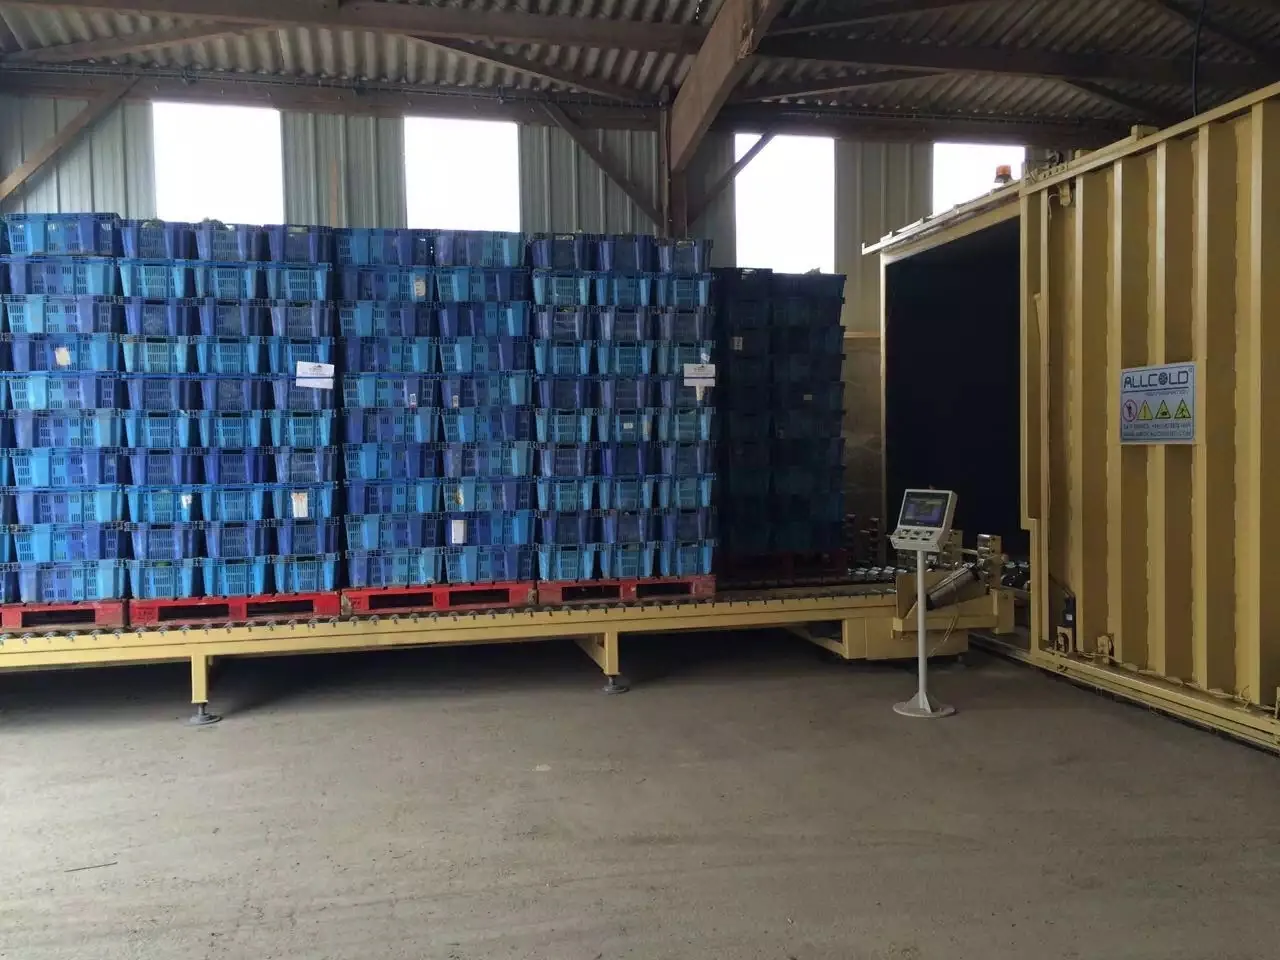
If handling is the measured bottleneck, compare manual loading with a specified conveyor arrangement. Confirm load stability, door interfaces, controls and operator access before assuming that automation will improve the line.
From Manual Labor to Continuous Flow
Measure the time spent positioning, loading, unloading and clearing each batch. Forklift or trolley loading may be appropriate when it matches the production rhythm. Consider additional automation only where the measured constraint and project scope justify it.
For example, a continuous oven feeding a batch cooler may need an accumulation area to collect each load and a buffer before packing. This is a planning scenario, not an Allcold delivery case. The complete arrangement and any automated interfaces require engineering review.
Compare these handling concepts as project options, rather than treating them as a standard Allcold automation package:
- Manual loading: assess forklift or trolley movement, staffing and cycle turnaround.
- Conveyor-assisted loading: define the mechanical interface and control responsibilities.
- Integrated handling: obtain a complete line design and separate supply scope; this is not implied by a standard cooler quotation.
| Handling concept | Evaluate | Scope to confirm |
|---|---|---|
| Manual | Measured loading and unloading time | Access, staffing and safe movement |
| Conveyor-assisted | Actual bottleneck and interface | Mechanical and control engineering |
| Integrated line | Buffers and peak operating pattern | Equipment, integration and acceptance responsibilities |
How Do You Synchronize Cooling Cycles with Your Production Rate?
Sometimes your production line outpaces your cooler, creating a pile-up. Other times, the cooler sits empty. This mismatch creates constant bottlenecks and makes your workflow unpredictable.
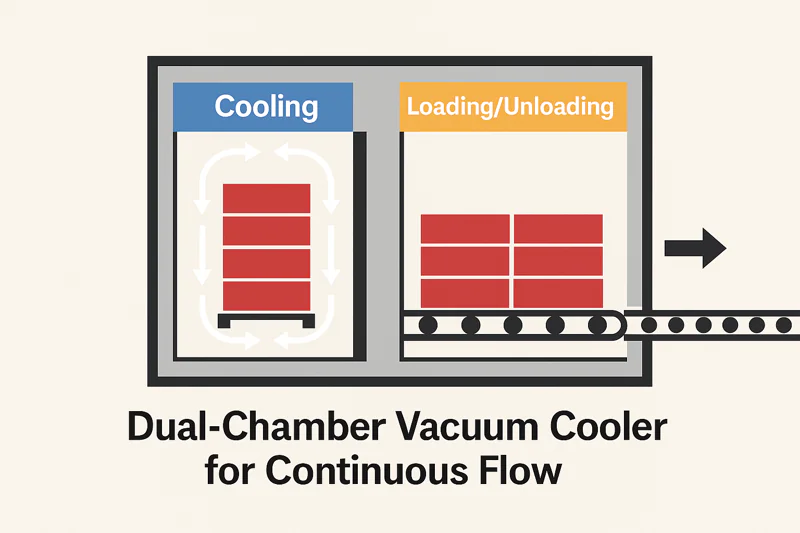
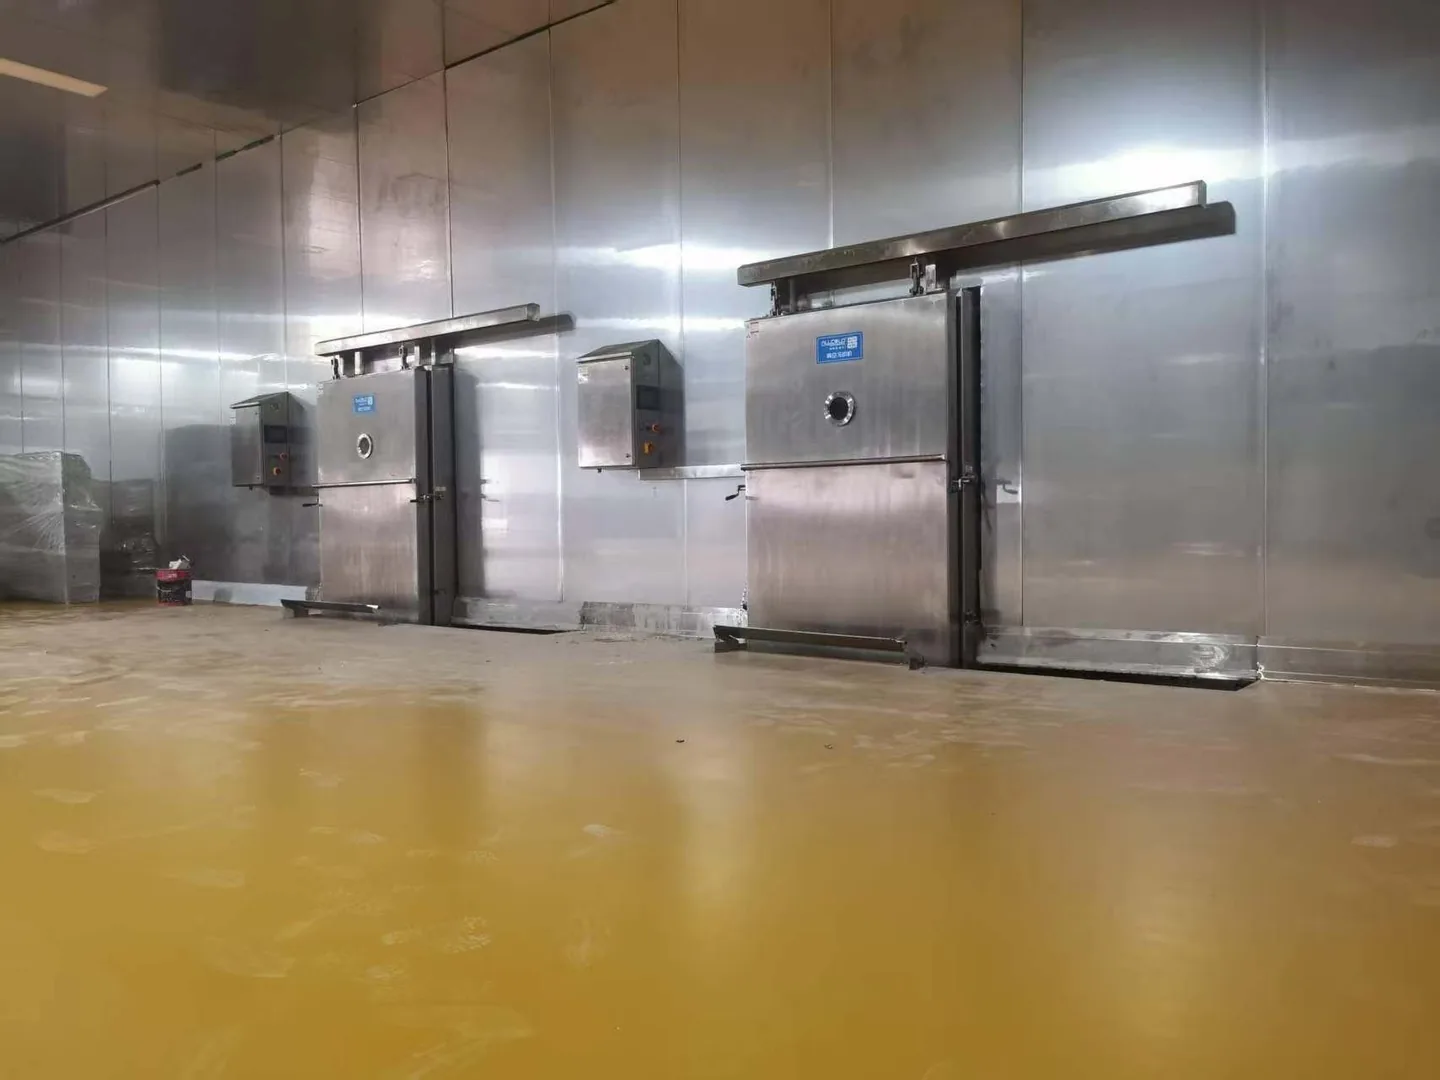
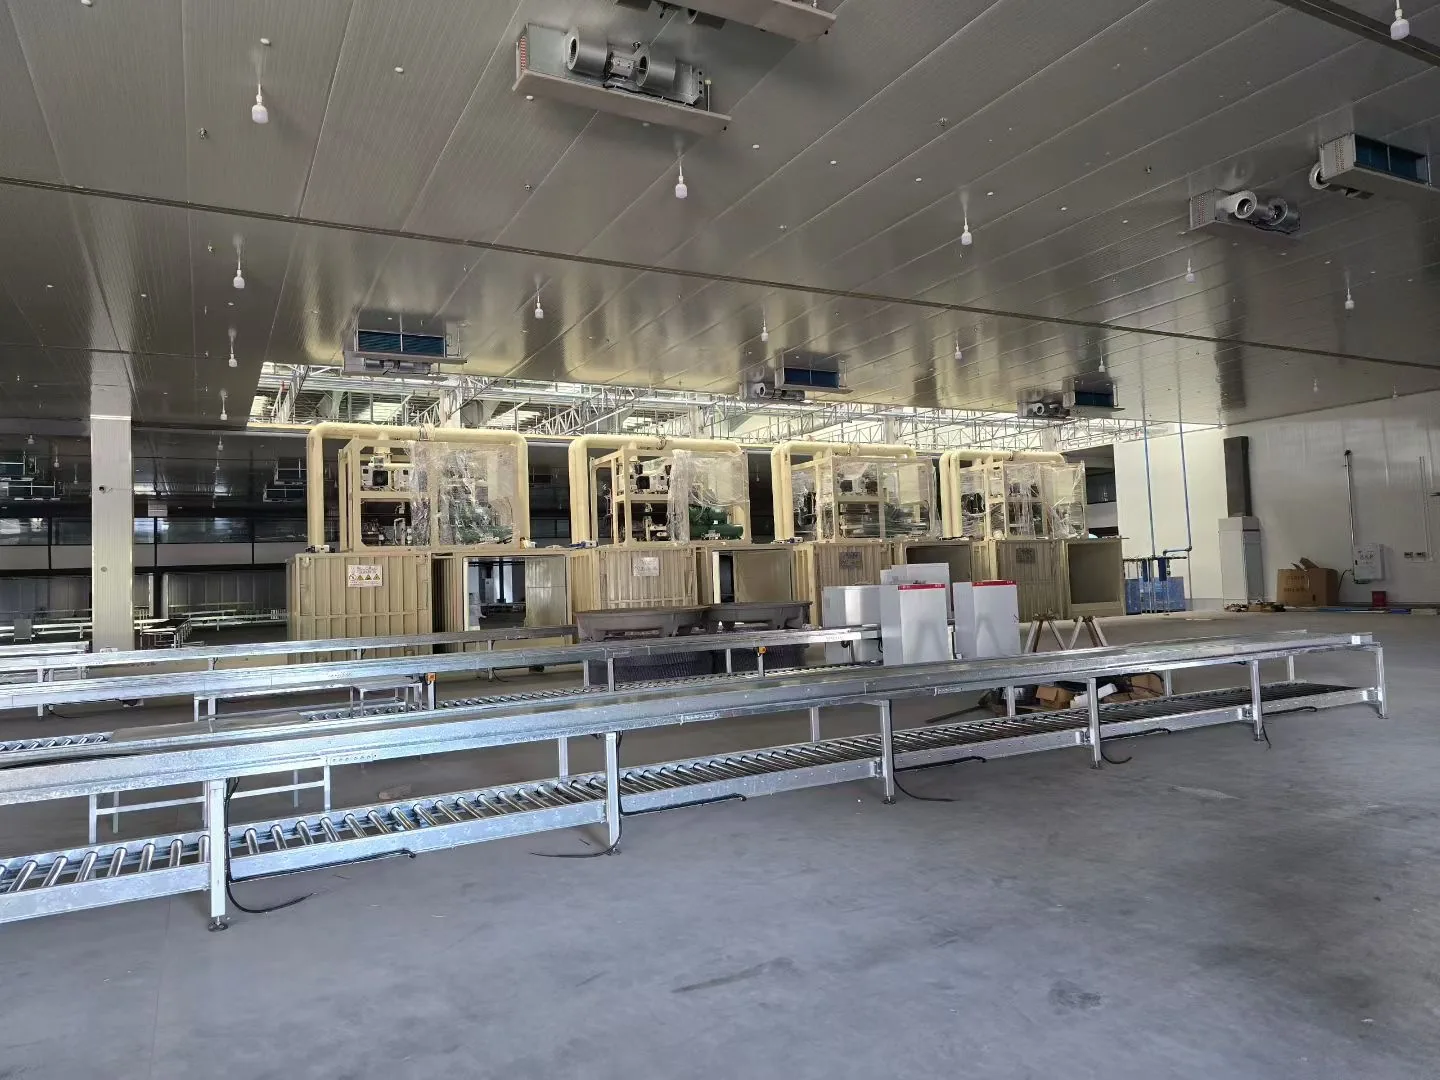
Size cooling against complete batch turnaround and peak arrivals. Two chambers may allow some handling to overlap with cooling, but the actual benefit depends on shared equipment, controls and the rest of the line.
Matching the Heartbeat of Your Production
Your production line5 has a certain rhythm, or "heartbeat"—the number of units or pallets it produces per hour. Your cooling system must match this rhythm perfectly. If your cooler is too slow, product piles up. If it’s too fast (or too large), it sits idle, wasting energy and capital. Synchronization is about doing the math before you buy.
Illustration: two pallets in a complete 20-minute turnaround would give six pallets per hour before interruptions. If 20 minutes describes cooling alone, loading, unloading and other stages reduce that rate. Use measured or agreed complete-cycle time and include a realistic operating allowance.
For a two-chamber proposal, confirm whether vacuum or refrigeration equipment is shared and which stages can run simultaneously. Compare the approved sequence and maintenance implications. Two chambers do not automatically provide continuous flow, fault redundancy or zero waiting.
| Question | Single chamber | Two-chamber proposal |
|---|---|---|
| Complete throughput | Include loading and unloading | Confirm which stages can overlap |
| Shared equipment | Identify its duty | Confirm limits on simultaneous operation |
| Maintenance | Plan access and downtime | Do not assume fault independence |
| Selection basis | Actual arrival pattern | Measured need for overlap or capacity |
How Can You Integrate Cooling Data into Your Factory’s Management System?
Your cooler is a ‘black box.’ You don’t know the exact cooling times or final temperatures for each batch, making it impossible to guarantee quality control or provide compliance data.
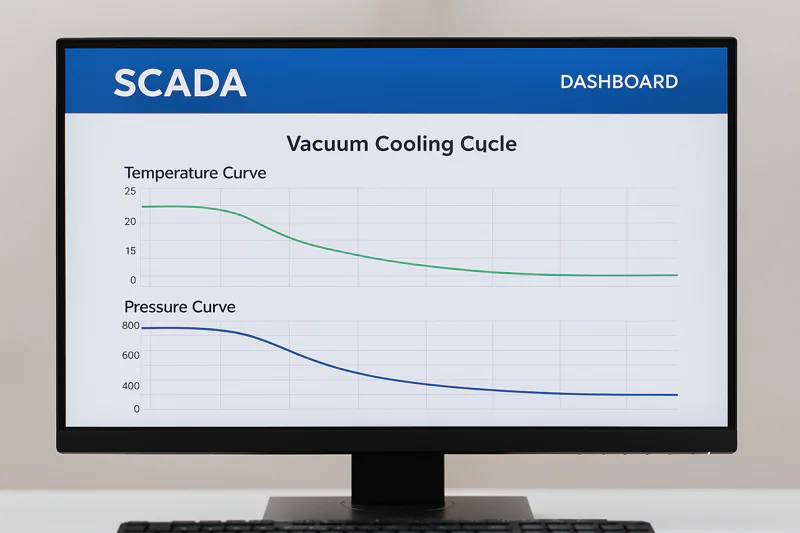
Historical records, file exports and SCADA connections are project-specific functions. Define the required fields, interface, retention and responsibilities, then confirm the delivered scope. A live HMI display does not establish that cycle data is stored or exported.
Turning Your Cooler into a Smart Device
Start with the records the production and quality teams actually need. Manual records or separate instruments may be sufficient for some workflows; automatic integration should solve a defined requirement rather than being assumed necessary.
Allcold’s confirmed baseline includes PLC/HMI control, live values, alarms, automatic/manual modes and password protection. Vegetable machines normally use two product probes. Wireless sensors, extra channels, batch identifiers and automatic export require separate confirmation.
Where records are required, identify the batch, measurement location, instrument and approved acceptance criteria. Recorded data can support review, but a graph or export alone does not prove that the full load meets food-safety requirements.
| Record | Purpose | Requirement to confirm |
|---|---|---|
| Batch identifier | Connect observations to the load | Manual or automatic assignment |
| Product temperatures | Review specified sampling points | Locations, instruments and acceptance limits |
| Cycle duration | Assess complete turnaround | Start and end definitions |
| Trends or exports | Support diagnosis when needed | Actual logging and interface scope |
Conclusion
Proper workflow integration makes your cooler the heart of your production line. It transforms a standalone machine into a seamless asset that boosts your speed, quality, and overall efficiency.
Understanding pre-cooling can help you optimize freshness and quality in your produce. ↩
Exploring post-cooling techniques is essential for ensuring food safety and quality in cooked products. ↩
Understanding vacuum coolers can enhance your knowledge of efficient cooling systems in food production. ↩
Explore effective strategies for workflow optimization to improve efficiency in your operations. ↩
Discover why synchronizing production lines is crucial for maximizing efficiency and minimizing waste. ↩
Learn about the vacuum cooling cycle and its importance in maintaining product quality and efficiency. ↩
Understand the key factors that influence the cooling process and how to optimize it for better results. ↩
Explore the advantages of dual-chamber vacuum coolers for continuous production flow in high-speed environments. ↩
Interested in vacuum cooling for your operation?
Mila
You May Also Like
Vacuum Cooler Water Quality: What to Check Before Connecting the Supply
Identify the water circuits, review a representative water analysis and clarify the utility scope before connecting a vacuum cooler. A practical guide for Allcold equipment buyers.
Buying a Vacuum Cooler for a Cold Climate? Plan for the Hours It Is Off
A winter specification should cover more than the temperature during production. Compare running, idle, power-loss and restart conditions before choosing the equipment.
Can a Vacuum Cooler’s Chamber, Pump and Chiller Go in Different Rooms?
Keep the chamber convenient for production without assuming the machinery must sit beside it. A practical guide to reviewing a split vacuum cooling installation.
Vacuum Cooling Sweet Corn: Look Beyond Cooling Speed
Can sweet corn be vacuum cooled? Compare moisture control, husk and pack formats, hydrocooling alternatives, and the product checks to agree before buying.
Vacuum Cooling Celery: Is It the Right Choice for Your Packing Line?
Can celery be vacuum cooled? Compare vacuum, hydro and forced-air cooling, then assess packaging, temperature, weight loss and real packing-line throughput.
Does a Bigger Vacuum Pump Mean Faster Vacuum Cooling?
Does a larger vacuum pump cool produce faster? Compare m³/h ratings, loaded cooling time and complete batch throughput before buying a vacuum cooler.
Which Refrigerant Should Your Vacuum Cooler Use?
Choosing a vacuum cooler refrigerant? Check local service support, destination rules, system performance and quotation details before ordering.
Can Your Floor Support a Vacuum Cooler? Look Beyond Tonnes per Square Metre
Check vacuum cooler floor loading before you buy: operating weight, support reactions, forklift wheel loads, ramps and the site data your engineer needs.
Buying a Vacuum Cooler Near the Coast? Specify More Than Paint
Coastal protection is more than chamber paint. Use this component-by-component checklist to compare vacuum cooler quotations, test evidence and maintenance scope.
50 Hz or 60 Hz? How to Confirm a Vacuum Cooler Will Work at Your Site
Buying a vacuum cooler for 50 Hz or 60 Hz power? Check whole-machine compatibility, auxiliaries, conversion scope and quoted performance before ordering.